Silicon Carbide Rod Standard Operation & Inspection Checklist
Silicon Carbide Rod Standard Operation & Inspection Checklist
WhatsApp: +8615804230746
Scope of Application: Box furnaces, muffle furnaces, tubular high-temperature electric furnaces equipped with silicon carbide (SiC) rod heating systems
Core Forbidden Operations (Strictly Prohibited): Rapid heating & rapid cooling; powering on damp furnaces; operating above 1400℃; energizing with loose wiring; heating materials containing sulfur, alkali, plastic or other corrosive substances
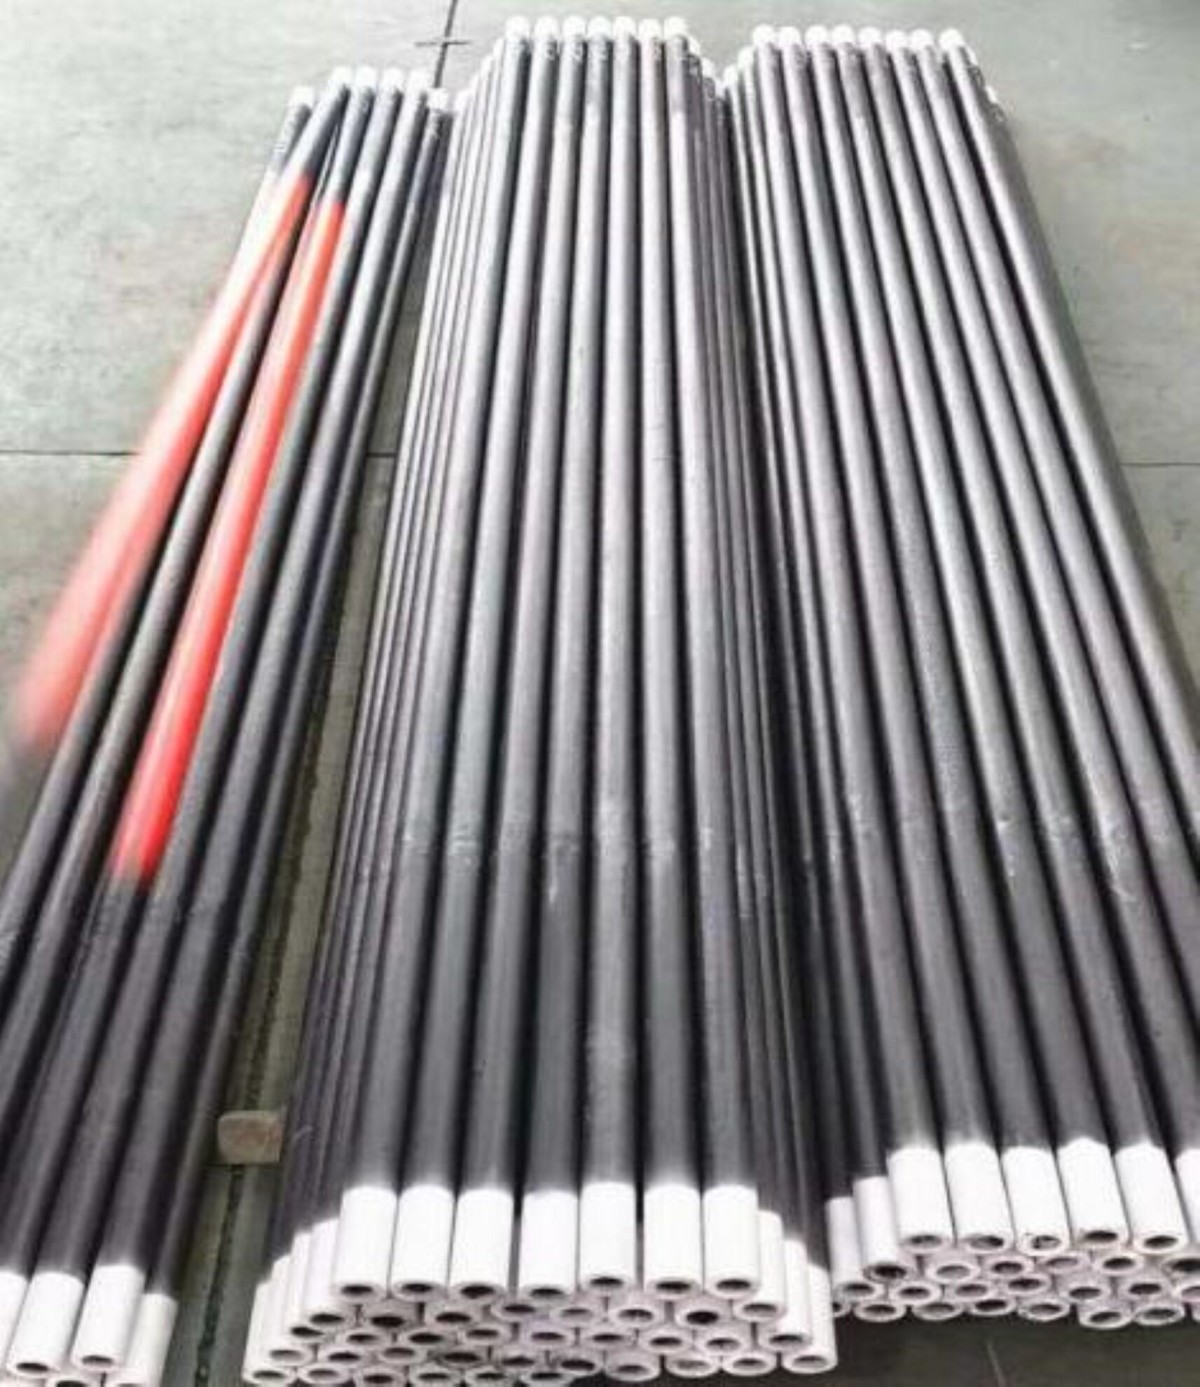
1. Pre-Start Inspection (Mandatory before power-on, check each item √)
1. Visual Inspection: No cracks, local whitening/thinning, partial blackening or bending deformation on SiC rods; intact aluminum conductive coating on both cold ends without peeling off
2. Mounting Gap Check: Sufficient reserved gap between rod body and furnace wall holes; no close contact with furnace wall; rods can expand and contract freely at high temperature without jamming or extrusion damage。
3. Wiring Inspection: Aluminum braided wires and terminal clamps are tightly fastened without looseness or spark oxidation marks; matched resistance for rods in the same group; mixed use of new and old rods in one group is forbidden
4. Furnace Internal Environment: No dust, workpiece debris or water moisture inside the furnace chamber; mandatory oven drying for new furnaces or furnaces shut down for more than 3 days; direct high-power heating is not allowed
5. Electrical Equipment Check: No damage to voltage regulators, temperature controllers and circuit lines; voltage adjusted to zero before startup; reliable equipment grounding confirmed
2. Furnace Drying Procedure (Mandatory for New Furnaces & Long-term Shutdown Furnaces)
Note: Never dry damp furnaces with new SiC rods under full power. Follow the slow moisture removal curve strictly:
1. Room temperature → 200℃: Hold for 3 hours to completely discharge internal moisture (Moisture is the top cause of SiC rod cracking)
2. 200℃ → 600℃: Uniform heating for 4 hours, heating rate ≤ 8℃/min
3. 600℃ → Working temperature: Uniform heating for 2 hours; violent voltage rise is prohibited throughout the process
3. Standard Heating Startup Steps
1. Step 1: Low-voltage Startup: Set initial voltage to 50% of rated voltage; run no-load for 30 minutes and check uniform glowing of all rods
2. Step 2: Gradual Voltage Boost: Increase voltage slightly every 20 minutes after temperature stabilizes; one-time full voltage startup is strictly forbidden
3. Step 3: Constant Temperature Operation: Temperature limit in air environment: Max instantaneous temperature 1400℃; long-term stable working temperature ≤ 1250℃
4. Heating Rate Requirement: Overall heating rate shall not exceed 10℃/min to avoid thermal shock caused by drastic temperature change
4. Routine Inspection during Operation (Check every 2 hours)
1. Visual monitoring: Consistent glowing color of all rods; no local overheating bright spots, partial blackening or flickering glow
2. Terminal condition: No overheating, spark discharge or burnt odor on wiring terminals and clamps
3. Furnace operation rule: Avoid long-time furnace door opening and cold wind direct blowing to rod bodies to prevent fracture from thermal shock
4. Voltage compensation: The resistance of SiC rods rises gradually during service, leading to power attenuation. Adjust voltage slowly for compensation; sharp one-time voltage increase is forbidden
5. Standard Shutdown Procedure (Key to Extend Rod Service Life)
1. Step 1: Reduce voltage to zero gradually, then cut off heating power supply
2. Step 2: Open furnace door for heat dissipation only after furnace temperature drops below 600℃
3. Forbidden Operation: Never open the furnace door fully when temperature is above 600℃. Direct cold wind impact will cause instant fracture of SiC rods due to severe thermal stress
6. Common Faults & On-site Emergency Solutions
7. Daily Storage & Replacement Guidelines
• Store spare SiC rods in dry and ventilated environment; damp rods are prone to cracking once powered on
• Replace rods only after full power cut and complete furnace cooling; hot disassembly and assembly are prohibited
• Replace rods as a whole group with consistent resistance; mixed new and old rods will cause overload burnout of new rods
• Continuous furnace operation is recommended; frequent startup and shutdown will greatly shorten the service life of SiC rods
Why your Silicon Carbide RodsBreak Easily
Silicon carbide heating rods are sintered ceramic components featuring high hardness but brittleness, prone to cracking from thermal shock or mechanical stress. Breakage mainly falls into five common causes related to production, installation and operation:
1. Sudden drastic temperature change (the top cause of breakage)
SiC rods have noticeable thermal expansion and contraction rates.
· Cold air rushing into the furnace when opening doors at high temperature, or feeding cold raw materials directly into hot chambers triggers abrupt local shrinkage and cracking.
· Rapid furnace shutdown and forced cooling, plus frequent start-stop cycles generate internal thermal stress and fractures.
2. Improper installation stress
1. Over-tightened clamps: rods expand slightly when heated; pre-tightened clamps restrict thermal expansion and cause rupture under high temperature.
2. Suspended cold ends or furnace vibration bend and snap rods during operation.
3. Forced fitting of mismatched-length rods creates hidden cracks that expand and break upon heating.
3. Electrical overload burnout
· Excessive input voltage and overloaded surface power lead to localized overheating and cracking/melting.
· Unbalanced three-phase load causes single rod overload failure.
· Aged rods with increased resistance concentrate heat in the hot zone and fracture due to uneven heating.
4. Corrosion and dust erosion inside furnaces (common in mining & metallurgy)
· Volatile alkaline metals, lead/zinc fumes and sulfur vapor from ore penetrate rod pores at high temperature, eroding grain boundaries and embrittling the material.
· Falling furnace charge and material impact cause physical breakage.
5. Poor raw material quality & mixed old/new rods
· Low-density inferior SiC rods with abundant inherent pores are naturally fragile.
· Mixing new and used rods: new rods have lower resistance and higher current/heat output, while aged rods carry uneven heat load, resulting in successive fractures (frequent failure on mine fire assay furnaces).
Practical Anti-break Tips
1. Slow heating rate: heat gradually from ambient to 600℃; avoid abrupt cooling.
2. Leave expansion clearance for clamps; never fasten completely tight.
3. Match rods from the same production batch with consistent resistance; prohibit mixing new and old units.